A few habits make parts come off the printer the way they were designed: lay them flat, leave room where parts fit together, and print a test or two to learn what your printer needs.
Lay it flat
Print a part on its largest flat face, so it needs little or no support. Right-click that face and choose Lay Flat on This Face, or choose Modify ▾ › Lay Flat on a Face… and click it. D drops the selection onto the plate.
Clearances are built in
Printed holes come out a little small and printed pegs a little big, so the parts that fit together leave room:
- Threads are cut 0.1 mm clear on each surface: a threaded cylinder a little thinner, a threaded hole a little wider. Change it with Clearance in the inspector's Thread section.
- Nut traps are 0.15 mm bigger on each side than the nut.
- Screw holes use the standard medium clearance for their screw size.
- Gears' teeth are 0.05 mm thinner on each face, so they mesh without binding.
These printed true in Caliper3D's own test prints. If your fits come out too tight or too loose, print the Fit Test below and change the clearance to suit.
Test prints
File › New from Template… (⇧⌘N) has three prints under Calibration & Tests:
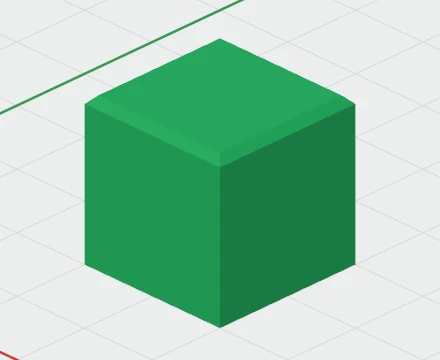
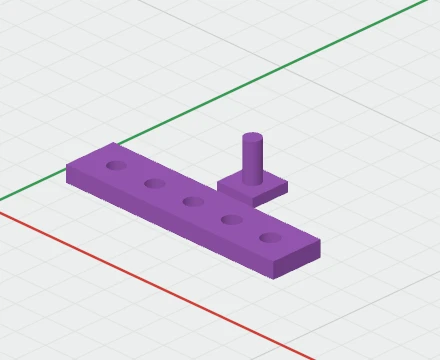
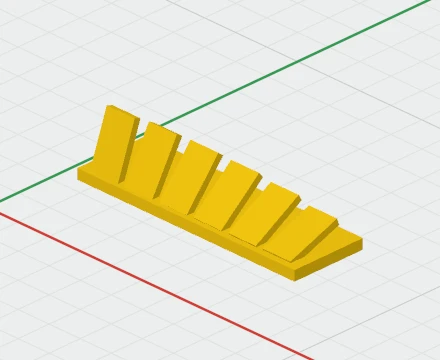
- Calibration Cube: 20 mm on every side. Measure the print to check your printer's sizes.
- Fit Test: holes from 5.0 to 5.4 mm, and a 5 mm peg. The tightest hole the peg slides into is the clearance your printer needs.
- Overhang Test: fins leaning 20° to 70° from upright, to see how far your printer can lean a wall before it needs support.
Before you export
- Holes cut only when grouped with the solids they're in. A loose hole is left out of the export.
- An object outlined in red stripes couldn't be made into a solid: the inspector says why.
- The note after exporting lists anything left out: see Exporting for Your Slicer.